PCB Design ServicesSchematics, Layout and Design for Manufacturing
2 to 8 layer boards, impedance control, mixed signal and EMC. Shenzhen, since 2016.
Service Overview
End-to-end PCB design from schematic capture to GERBER release. 2 to 8 layer stackups, impedance-controlled routing for USB, MIPI DSI, LVDS and DDR, with complete production file output including silkscreen, pick-and-place and stencil.
XTELL provides PCB design services from schematic through 2-8 layer layout and impedance control to complete production files, including high-speed and mixed-signal boards.
Who this PCB design service is for
• Companies with a new product that needs taking from schematic to production files: main controller, power and peripherals settled, then straight into prototyping.
• Clients revising an existing board: swapping components, fixing signal problems, reducing size or cost.
• Clients whose high-speed or mixed-signal boards are hard: a fast main controller, high-precision analog sensing, and routing that cannot rely on luck.
From schematic to production files: what the delivery chain looks like
PCB design delivers not a drawing but a complete file package ready for production. The RK3128 mainboard project is the standard example: GERBER files, silkscreen, pick-and-place coordinates and stencil files, updated in step with each revision. Schematic, layout and production files all pass through the same team, with no hand-off to different people or tools in between, so versions never drift out of sync.
Case one: the RK3128 mainboard, high-speed signals and power integrity
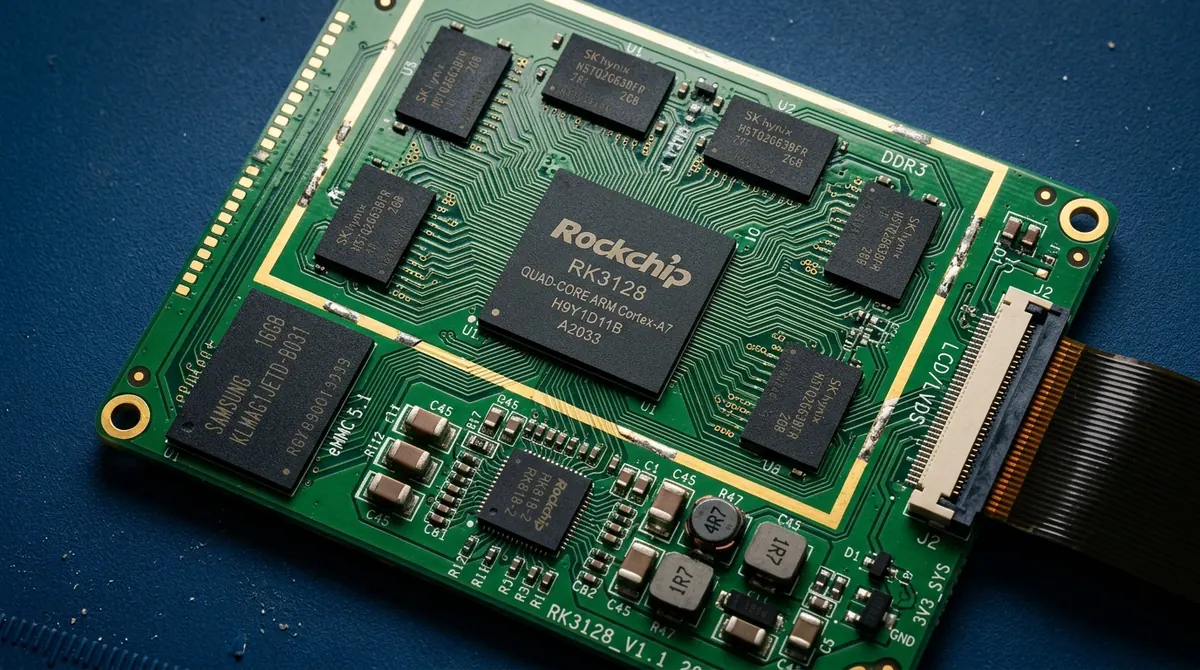
The hard parts of the RK3128 mainboard were high-speed signal integrity, power integrity, and managing iteration across board revisions. Layout and routing were refined over several revisions, an LCD driver board was adapted to different screens, and a debugging log recorded each revision's problems and fixes. On an SoC mainboard like this, the design centres on the power tree and timing-critical signals: if the supply is unstable or a key bus is routed badly, no amount of software tuning will recover it.
Case two: the USB Type-C development board, MUX replacement and signal integrity
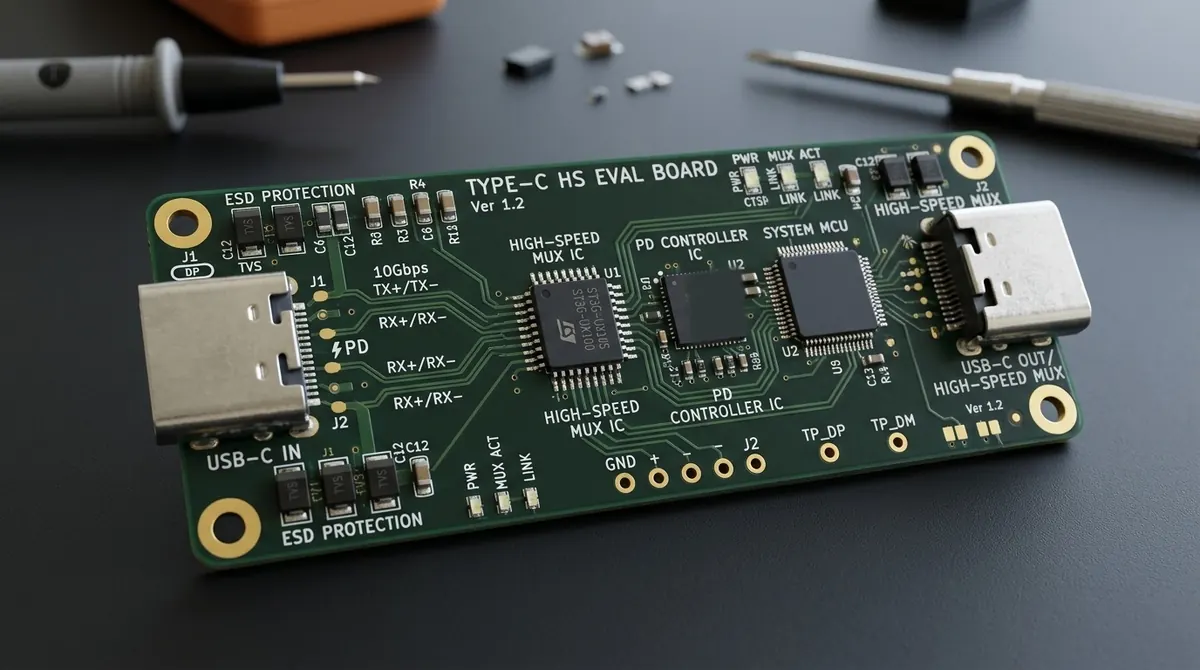
The challenge on the USB Type-C development board was replacing the Type-C MUX reliably without losing signal integrity. The work covered selecting an alternative MUX device, designing both dual-port and single-port boards, and verifying against the reference design. Type-C high-speed lanes are sensitive to the MUX, trace length and via placement, so a replacement is not done when the board powers up - it has to be verified to show no loss of performance. The project is also a direct example of component-substitution work, whether for cost-down or an out-of-stock part.
Case three: the human body posture sensor, multi-sensor mixed-signal design
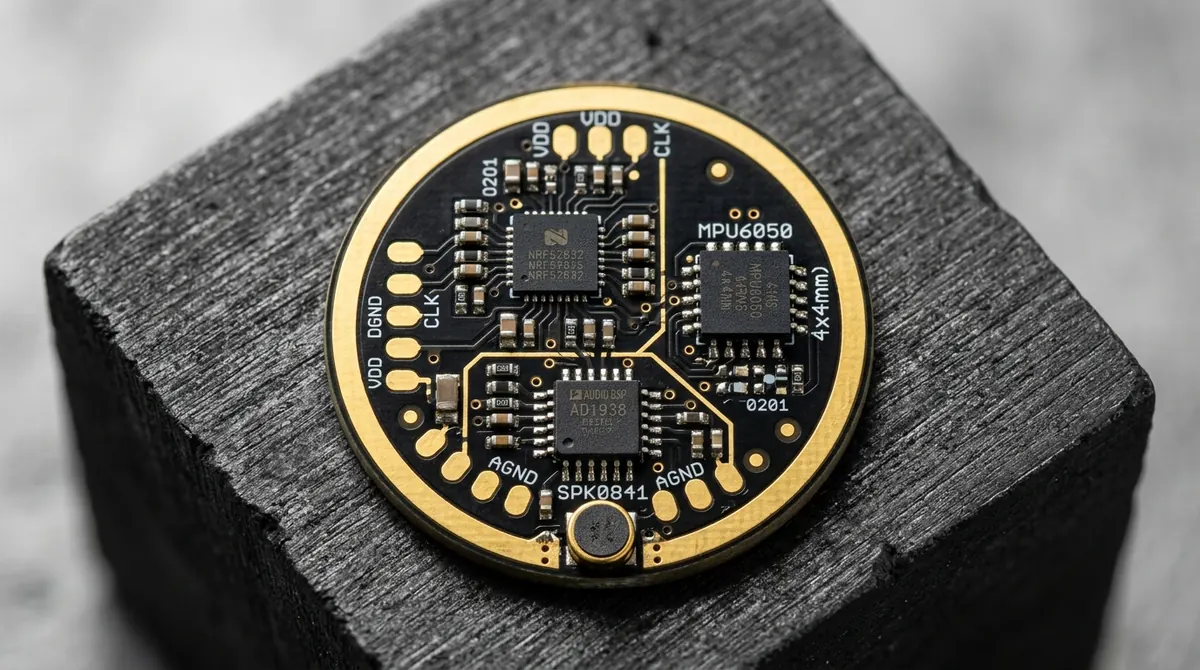
The human body posture sensor is a typical small mixed-signal board. A BLE MCU processes data from three inertial sensors - MPU6050, SC7A20 and STK8321 - a dedicated audio processor handles noise reduction and keyword spotting, a ring buffer manages real-time data, BLE connects to the phone, RFID handles identification, and a WeChat mini program provides remote control and data display. The challenge was integrating several sensors and audio processing for use in sport while keeping power low and response real-time. With digital, analog, RF and audio on one board, keeping each region from disturbing the others is the core of the layout.
What matters in high speed PCB design
High-speed design succeeds or fails on two things: power integrity and signal integrity. Can the power distribution network hold the voltage through load steps, and are the critical traces impedance-controlled, length-matched and referenced to a solid plane? The RK3128 mainboard was iterated across revisions along exactly these two lines. Honestly, a first revision of a high-speed board is rarely perfect, so multi-revision iteration and per-revision debugging logs are part of the process. We do not promise it will pass first time; we promise that every revision records what changed and why.
Mixed signal and analog circuits: how noise isolation is done
The core tension on a mixed-signal board is that digital switching noise couples into analog sampling and eats the sensor's effective bits. The posture sensor board is partitioned: sensor analog, audio processing, digital control and BLE RF regions each get their own placement and return paths, and sensitive analog signals never run parallel to high-speed digital lines. ADC and DAC boards follow the same rule - sampling accuracy ultimately comes down to layout, not the chip's datasheet.
Multi-revision iteration and debugging logs are part of the delivery
PCB design is naturally a multi-revision process. The RK3128 mainboard went through several rounds of layout and routing refinement, with each revision's problems and fixes entered in a debugging log. That log pays off at hand-over: whoever receives the board knows why each jumper exists and what each revision corrected. Iterating without records just leaves the old problems for the next revision to rediscover.
Design tool: KiCad
PCB design is done in KiCad. We do not depend on paid EDA software, and GERBER and production files are not tied to a particular toolchain, so any fab can work from them. Whether the source files for schematic and layout are delivered, and how they are licensed, is agreed per project in the contract - this page makes no blanket commitment.
PCB design and firmware debugging sit with the same team
Whoever drew the board debugs its firmware. At XTELL one team writes the firmware, the app and the backend. When a peripheral misbehaves we check the schematic and put a scope on the signal to decide whether it is a layout problem or a driver problem, and change the next revision of the board if needed. The RK3128 mainboard converged quickly across revisions because design and debugging were in the same hands - across companies, every revision costs another round of emails.
Certification decisions are made at the layout stage
Clients' products routinely need FCC or CE certification, and XTELL supports the certification work. The PCB decisions with the biggest effect on certification are made at layout: RF routing and antenna keep-out, power filtering and ground plane integrity. Thinking about certification after layout is fixed costs far more in revisions than getting it right from the start. Certificates are issued by accredited test labs; our job is to make the design pass first time.
How design hands over to prototyping and trial production
Fabrication, assembly, DFM checks and iteration after the design is finished fall under the PCB prototyping and trial production service - this page gets the design right, that one gets the board built. The two connect without a gap: production files come out of this page's work, and trial-production problems flow back here for revision. You can engage for design only, or for design through trial production, as agreed per project in the contract.
About XTELL
XTELL (Shenzhen XTELL Future Technology) was founded in Shenzhen in 2016. Over the ten years since, it has delivered more than 100 projects, with clients predominantly western B2B companies. Its work covers every layer from circuit board to cloud: PCB design, FPGA, embedded firmware, Linux BSP, device interfaces, mobile apps, backends and IoT platforms.
Service Features
Technology Stack
Related Project Cases
RK3128 Mainboard Hardware Design
Multi-version PCB iteration on an RK3128 SoC mainboard with LCD driver adaptation. Full production output: GERBER, silkscreen, pick-and-place and stencil files.
USB Type-C Development Board
Dual-port and single-port Type-C board designs around a PD controller and a high-speed MUX, including an alternate-device solution verified against the reference design.
Human Body Posture Sensor
BLE MCU board carrying MPU6050, SC7A20 and STK8321 MEMS inertial parts alongside an audio path, BLE radio and RFID - a dense mixed-signal layout where sensor placement, antenna keep-out and return paths decide whether the data is usable.
What You Receive
Frequently Asked Questions
How many layers do you design?
2 to 8 layer layout is within this service. Layer count is set by signal density and power integrity needs, and more is not better - two extra layers raise material cost, so we recommend a layer count with reasons at the design stage.
What do the production files include?
A complete set: GERBER, silkscreen, pick-and-place coordinates and stencil files, the standard the RK3128 mainboard project was delivered to. On multi-revision work every file is updated and version-marked together, so you never get a new drawing with old coordinates.
What real high-speed boards have you done?
The RK3128 mainboard: SoC high-speed signal and power integrity design, multi-revision iteration, and an LCD driver board adapted to several screens. The USB Type-C development board: MUX replacement on high-speed lanes with signal integrity verified against the reference design. Both were proven through real iteration, not on paper.
Do you design RF boards?
We have delivered boards with RF: the posture sensor board integrates BLE RF around a BLE MCU. Higher frequency bands and more complex RF front ends are assessed per project - if it is outside what we can do, we will say so rather than take it on.
Do you deliver the schematic and PCB source files?
We work under both open and closed models. Whether design files are part of the delivery, and how they are licensed, is agreed per project in the contract and written down before signing. This page makes no blanket commitment; tell us your preferred model at the quoting stage.
Do you handle fabrication and assembly?
Fabrication, assembly, DFM checks and trial-production iteration fall under the PCB prototyping and trial production service, which runs on from design. You can engage for design only or for design through trial production, with the boundary agreed per project in the contract.
Need Professional Services?
Contact us for customized solutions and quotes