PCB Prototyping and Pilot RunsFrom Files to a Production-Ready Board
Fast fabrication, assembly, DFM review and multi-revision iteration. Shenzhen, since 2016.
Service Overview
XTELL takes boards from manufacturing files to a production-ready revision: fast fabrication, assembly, DFM review, BOM optimisation and multi-revision iteration, handled as one continuous engagement.
XTELL provides PCB prototyping and pilot run services: fast fabrication and assembly, DFM review and BOM optimisation, iterated over multiple revisions until the hardware is ready for a pilot run.
Who this prototyping and pilot run service is for
• Companies whose design is ready and who need real boards fast: schematic and layout are fixed, and someone needs to tie fabrication, assembly and first-article bring-up together.
• Clients whose prototype works but whose pilot run fails: five of ten assembled boards are bad, parts cannot be sourced or soldered, boards warp and components tombstone, and someone needs to solve the manufacturability problems.
• Teams in the middle of multi-revision iteration: every revision means new output files, orders, tracking and testing, and nobody in-house has the time to follow it all.
• Clients whose product has to reach production readiness: the goal is not a board that lights up, but an assembly line that runs cleanly at an acceptable yield.
What the full process from prototype to pilot run looks like
The process is a four-step loop: fast fabrication (manufacturing file output and fab tracking), then assembly (BOM sourcing checks, stencil and pick-and-place data matched to the revision), then test and fault isolation (first-article inspection, functional verification, defect records), then revision (problems fed back into the design for the next version). The loop runs until the pilot batch passes consistently - iterating to production readiness is how this service defines done. Design work is handled on the PCB design page; this page takes over from the manufacturing files.
Case one: the smart medication dispenser, power, audio and structure iterated together
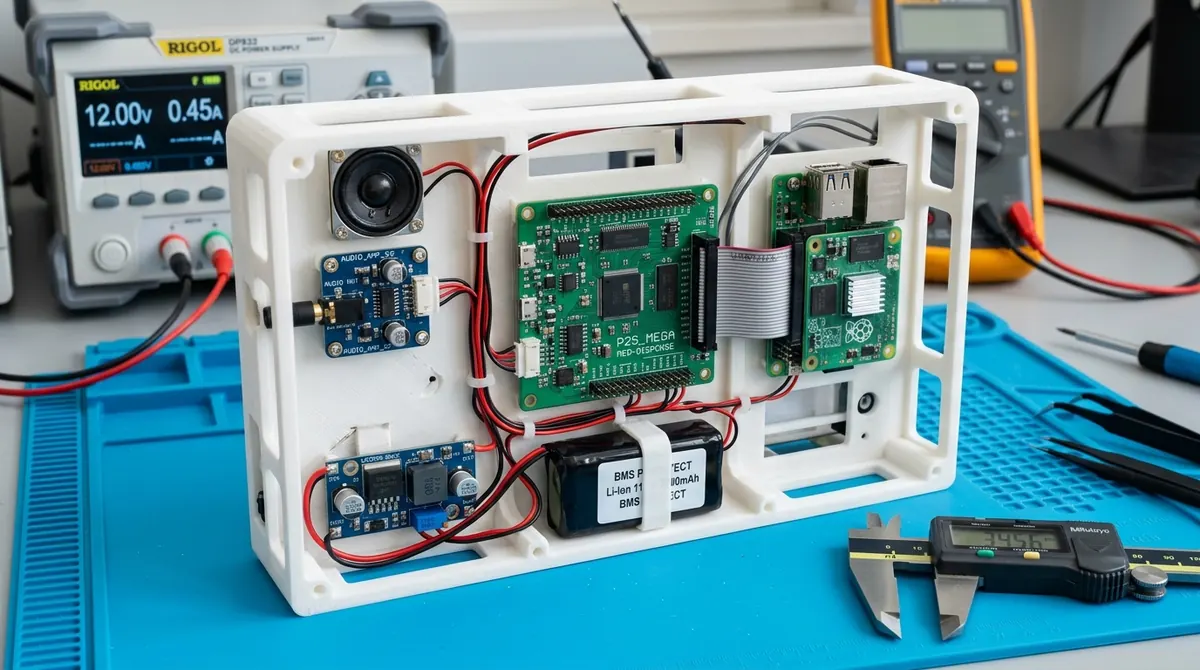
The smart medication dispenser is a typical whole-product prototyping project. A P25_MEGA main board carries the control logic, a Raspberry Pi is the main controller and a speaker amplifier board drives the audio; power management steps 12V down to 5V and supports both 1-cell and 3-cell battery configurations; the mechanical design produced the fd1_frame chassis. The challenge was getting the mechanical structure, power management and embedded control to work together reliably in one device. In an electromechanical product like this, pilot run problems never come from the board alone - mechanical interference and power margin are just as fatal.
Case two: the microscope motorized stage, iterating an electromechanical actuator
Iteration on the microscope motorized stage covered both the electronics and the mechanics. An ATMEGA32U4 runs 3CNC firmware, A4988 and HR4988E stepper drivers drive the motors, expanded through an Arduino CNC Shield; the stage PCB was designed alongside, and the structure was done in FreeCAD with STEP output. High-precision micro-motion is sensitive to both mechanical accuracy and the drive circuitry, so during prototyping every board revision was verified together with its mechanical parts - tuning either side alone never converges.
Case three: the FPGA plotter control system, multi-revision hardware optimisation
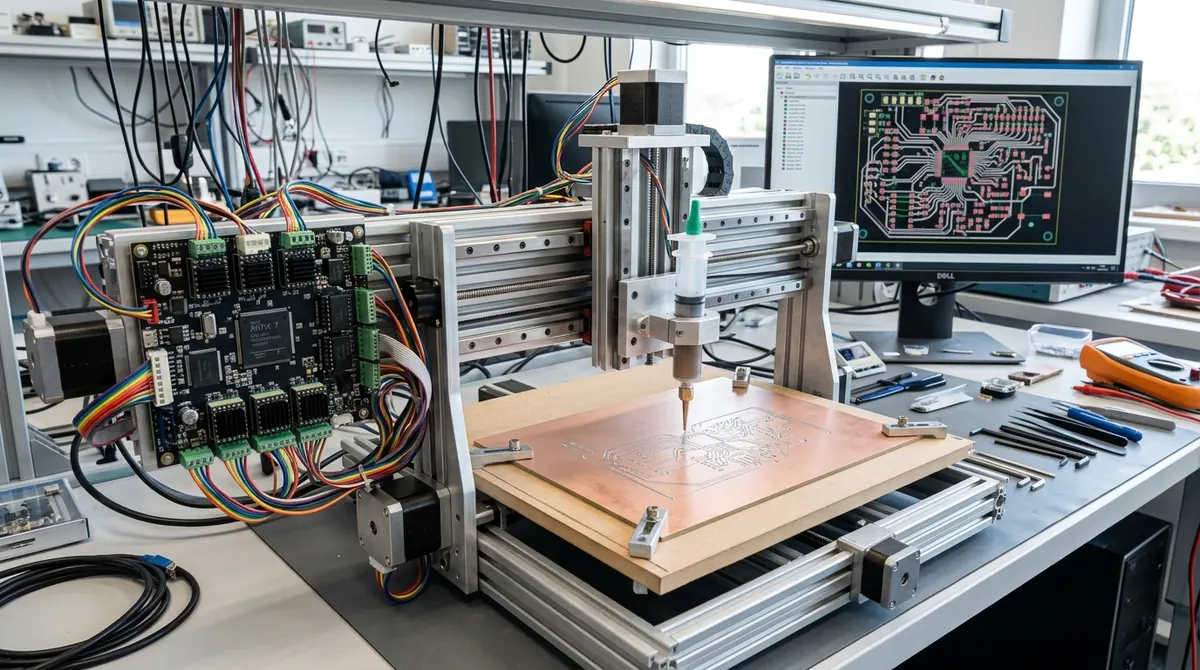
The FPGA plotter control system implements motion control logic on an FPGA and parses Gerber files as its graphics data source, for industrial automation. The development environment runs in a virtual machine, and the hardware was optimised over several revisions. What marks prototyping on a project like this: FPGA timing closure is tightly bound to board-level signal quality, so every pilot build goes back to comparing simulation with measurement. Multiple revisions are not compensation for failure; they are the normal development rhythm for this kind of system.
DFM review: the savings all happen before assembly
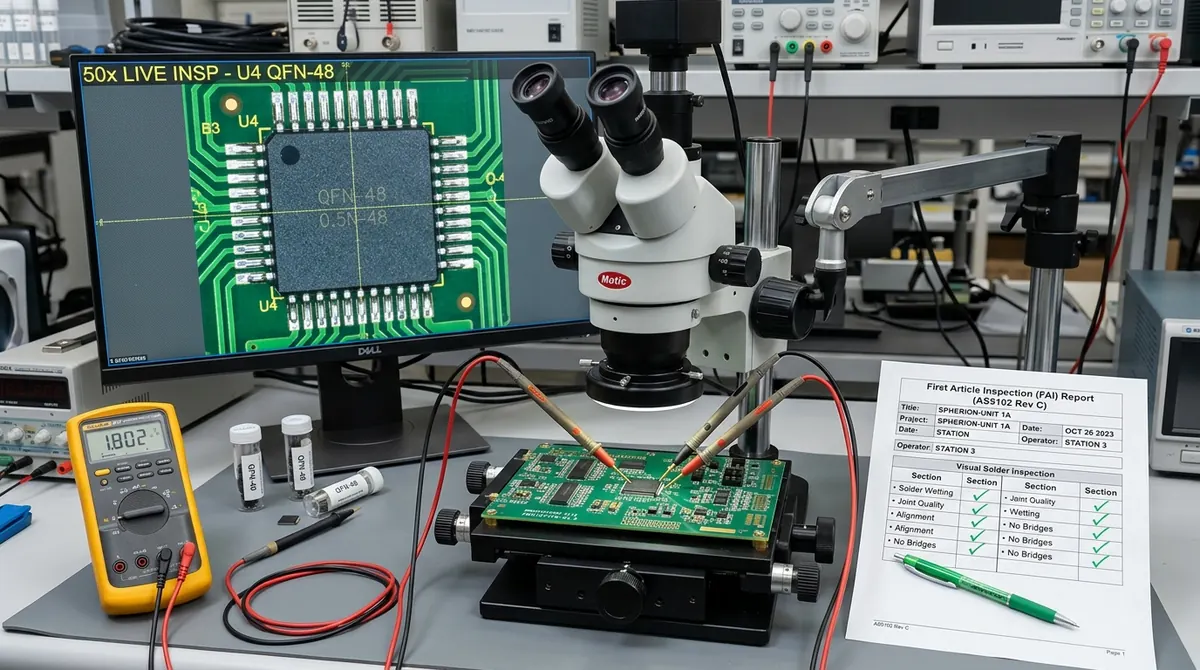
Design for manufacturing (DFM) review happens before the order is placed: do the pads match the stencil apertures, is there enough clearance between parts for the placement head, is the polarity silkscreen clear, have test points been left? A DFM change at the Gerber stage costs nothing; after assembly it means reworking the whole batch. DFM review is a fixed step of this service, and its checklist and conclusions are archived with the manufacturing files - each new revision starts by checking against the previous one's issue list.
BOM optimisation: part substitution and lead-time risk
BOM work falls into two kinds. The first is cost reduction - evaluating alternative parts with the same function, checking package compatibility and signal integrity together. The second is supply assurance - alternatives when a part goes out of stock. The smart medication dispenser's power section supports both 1-cell and 3-cell battery configurations, leaving room in the power BOM for different product variants. The rule of BOM optimisation: every substitution must pass three checks - performance, package and availability. Swapping parts on price alone just moves the risk onto the assembly line.
Multi-revision iteration: a pilot run is never a one-shot
All three cases reached their result through multiple revisions: the dispenser's structure and power were adjusted in step, the stage's board and mechanical parts converged together, and the plotter's FPGA hardware was optimised version by version. The discipline of the pilot stage is version control - what changed in each revision, why, and what verification concluded, all on record. Iteration without records means leaving problems already solved for the next revision to discover again.
Firmware bring-up on the prototype does not need a third party
Boards back from prototyping are brought up by XTELL's own firmware engineers: the dispenser's control logic runs on the Raspberry Pi and the stage's 3CNC firmware runs on the ATMEGA32U4. When first-article inspection finds a problem, the firmware side can help isolate it immediately, separating soldering, component and design causes the same day. In the traditional model where prototyping and debugging are split, that round trip usually crosses another supplier and waits another cycle of communication.
Mechanics and enclosure iterate alongside the board
A pilot run is not only about the board. The dispenser's fd1_frame chassis and the stage's FreeCAD mechanical parts were designed and revised in step with their circuit boards. Board-to-board connector positions, mounting holes and height limits are aligned with the mechanics during layout - a board that passes testing but does not fit the enclosure is worthless.
Pilot run preparation before certification
Clients' products routinely need FCC, CE or similar certification, and XTELL supports the related work. Certification preparation during the pilot stage means consistency across the certification batch, confirming that RF and power-related revisions have converged, and having the builds and documentation the test lab requires. Certificates are issued by accredited test labs - one goal of pilot iteration is making sure design problems do not first surface on the certification test bench.
How this connects with the PCB design service
Once the design is complete on the PCB design page and the manufacturing files are out, this page takes over fabrication, assembly, DFM, BOM and iteration. Clients can also engage for the pilot side only - they provide finished design files and we start from DFM review. Whether we take on design through pilot run or only one part is agreed per project in the contract; whether source code and design files are delivered, and under what licence, is likewise written into the contract item by item, and nothing on this page constitutes a blanket commitment.
About XTELL
XTELL (Shenzhen XTELL Future Technology) was founded in Shenzhen in 2016. Over the ten years since, it has delivered more than 100 projects, with clients predominantly western B2B companies. Its work covers every layer from circuit board to cloud: PCB design, FPGA, embedded firmware, Linux BSP, device interfaces, mobile apps, backends and IoT platforms.
Service Features
Technology Stack
Related Project Cases
Smart Medication Feeder
P25_MEGA main board with Raspberry Pi control logic, a speaker amplifier board, 12V to 5V power management, 1CELL/3CELL battery supply and fd1_frame structural design.
Microscope Motorized Stage
Micro platform PCB with ATMEGA32U4 and A4988/HR4988E stepper drivers, delivered alongside STEP and FreeCAD structural design and an Arduino CNC Shield expansion.
FPGA Plotter Control System
FPGA-driven plotter control with Gerber file parsing for graphic data, taken through multi-version hardware iteration to optimise the design.
What You Receive
Frequently Asked Questions
How long does prototyping take?
It depends on the fab's schedule, layer count and process, and component lead times - if one part in the BOM is out of stock, the whole batch waits. At assessment we give an estimate based on current lead times; this page does not state a fixed number of days, because a fixed number means nothing in a shortage season.
Can you do small-batch assembly?
Yes. Assembly of the pilot batch is within this service, followed from stencil and pick-and-place data through first-article inspection. Volume manufacturing is carried by the client's manufacturing partners; we support the pilot run and fault isolation.
Will you optimise our BOM?
Yes. Cost-reduction alternatives and out-of-stock substitutes are both in scope, and every substitution passes the performance, package and availability checks before it enters the BOM. Parts the client specifies - a particular brand of main controller, for example - are kept as specified.
The design is our own. Can you do only DFM review and prototype management?
Yes. The client provides finished manufacturing files and we start from DFM review: the issues found are returned as a list, and you decide whether to change them and who does it. If you want us to take on the revisions as well, the work is estimated on the actual scope.
If the pilot run has problems, who is responsible for finding the cause?
Within the scope of this service, first-article inspection and defect isolation are ours: soldering, component and design causes are separated, and conclusions come with the data. Whether design revisions are in scope is agreed in the contract - when we take on design through pilot run together, there is no room for finger-pointing.
Do you deliver the design and manufacturing files?
We work under both open and closed models. Whether files are part of the delivery, and how they are licensed, is agreed per project in the contract and written down before signing. This page makes no blanket commitment; tell us your preferred model at the quoting stage.
Need Professional Services?
Contact us for customized solutions and quotes